
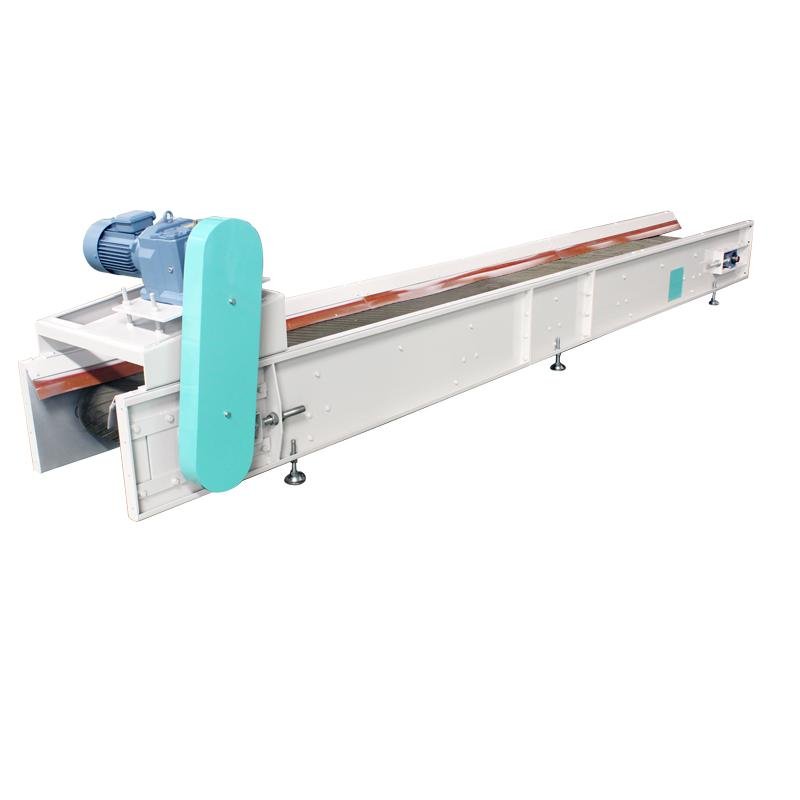
Descripción
Technical Specifications & Design Variations
Belt Types & Characteristics
-
Fabric Belts: EP (Polyester-Nylon) 2-8 plies, strength 315-2000 N/mm
-
Steel Cord Belts: ST series, strength 1000-7500 N/mm for long distances
-
Heat Resistant Belts: Withstand temperatures up to 400°C
-
Oil Resistant Belts: Special compounds for lubricated materials
-
Food Grade Belts: FDA/USDA approved materials with white covers
Conveyor Structure & Components
-
Idler Types: Troughing, impact, return, training idlers
-
Idler Angle: 20°, 35°, 45° troughing configurations
-
Pulley Diameter: 200-2000mm based on belt tension and load
-
Construcción del bastidor: C-channel, truss, or channel stringer designs
Drive Systems & Power Requirements
-
Drive Power: 1.5-5000 kW depending on length and capacity
-
Drive Arrangements: Head, tail, or intermediate drives
-
Take-up Systems: Gravity, screw, or hydraulic tensioning
-
Braking Systems: Backstops, holdbacks, or disc brakes
Especificaciones de rendimiento por aplicación
| Aplicación industrial | Capacidad típica | Belt Speed | Incline Capability | Características especiales |
|---|---|---|---|---|
| Bulk Material Handling | 100-20,000 t/h | 1.0-5.0 m/s | Up to 30° | Dust containment, impact beds |
| Package Handling | 500-10,000 units/h | 0.5-2.5 m/s | Up to 15° | Zero-pressure accumulation |
| Mining & Quarrying | 500-40,000 t/h | 2.0-7.5 m/s | Up to 25° | Fire resistance, rip detection |
| Procesamiento de alimentos | 1-500 t/h | 0.3-2.0 m/s | Up to 20° | Sanitary design, washdown capability |
Parámetros operativos:
-
Belt Widths: 300-3000mm standard widths
-
Conveying Lengths: 5m to 15,000+ meters
-
Lump Size: Up to 1/3 belt width for standard applications
-
Rango de temperatura: -60°C to +400°C with specialized belts
Funciones avanzadas e integración tecnológica
Monitoring & Safety Systems
-
Belt Misalignment Switches: Automatic correction and shutdown
-
Rip Detection Systems: Steel cord sensor loops for early warning
-
Speed Monitoring: Encoder-based speed and slip detection
-
Pull-cord Switches: Emergency stop along entire conveyor length
Automation & Control
-
Variable Speed Drives: Energy optimization and flow control
-
PLC Integration: Centralized control with SCADA systems
-
Weighing Systems: Belt scales for continuous mass measurement
-
Detección de metales: Tramp metal protection for downstream equipment
Specialized Configurations
-
Curved Conveyors: Horizontal curves to navigate terrain
-
Pocket Belts: High-incline conveying up to 90°
-
Sandwich Belts: Vertical conveying without transfer points
-
Pipe Conveyors: Completely enclosed material containment
Aplicaciones específicas por sector
Mining & Bulk Handling
Belt conveyors form the primary transportation method in surface and underground mining operations. A single overland conveyor can replace hundreds of truck journeys daily, reducing fuel consumption by 80% and minimizing environmental impact. Modern mining conveyors regularly achieve capacities exceeding 10,000 t/h across distances of several kilometers.
Manufacturing & Assembly
In production facilities, belt conveyors provide synchronized movement of components through assembly processes. The consistent speed and positioning enable precise workstation timing and material presentation, reducing handling time and improving ergonomics.
Distribution & Logistics
Package handling conveyors form the circulatory system of modern distribution centers, with sortation systems capable of processing over 20,000 packages per hour. Advanced control systems route individual items to specific destinations with 99.9% accuracy.
Procesamiento de alimentos y bebidas
Sanitary belt conveyors handle everything from raw ingredients to packaged products, with designs that support frequent washdowns and prevent contamination. USDA-approved materials and easy-clean designs ensure compliance with food safety standards.
Economía operativa y mantenimiento
Análisis de costes
-
Inversión inicial: $500-$2,500 per meter depending on specifications
-
Costes de instalación: 20-40% of equipment cost for complex systems
-
Costes operativos: $0.50-$5.00 per operating hour depending on size
-
Costes de mantenimiento: 2-5% of initial investment annually
Métricas de eficiencia
-
Energy Consumption: 0.5-2.0 kWh per ton-kilometer
-
Availability: 95-99% with proper maintenance programs
-
Life Expectancy: 10-25 years depending on application and maintenance
-
Operating Efficiency: 85-98% of theoretical maximum capacity
Case Study – Cement Plant:
After implementing a 3.2km overland conveyor system:
-
Transportation costs reduced from $3.50 to $0.80 per ton
-
Annual maintenance savings of $450,000 compared to truck haulage
-
Dust emissions reduced by 95%
-
Availability of 98.5% over first three years of operation
Ingeniería de mantenimiento y fiabilidad
Programa de mantenimiento preventivo
-
Diario: Visual inspection, cleaning, belt tracking check
-
Semanal: Idler rotation, lubrication, wear inspection
-
Mensual: Pulley lagging inspection, belt splice examination
-
Anualmente: Complete system audit and component replacement
Critical Component Life
-
Belting: 3-15 years depending on application and maintenance
-
Idlers: 15,000-50,000 hours between replacements
-
Pulleys: 10-20 years with proper maintenance
-
Componentes de accionamiento: 7-15 years service life
Common Maintenance Issues
-
Belt Mistracking: Adjust idlers, check loading conditions
-
Material Spillage: Improve loading, install proper skirting
-
Idler Failure: Regular rotation and replacement programs
-
Belt Damage: Impact beds, proper loading chute design
Desarrollo futuro y tendencias del sector
Evolución tecnológica
-
Smart Monitoring: IoT sensors for predictive maintenance
-
Energy Recovery: Regenerative drives capturing downhill energy
-
Advanced Materials: Longer-lasting components and belting
-
Gemelos digitales: Virtual simulation for optimization and training
Sustainability Initiatives
-
Energy Efficiency: High-efficiency motors and optimized design
-
Reducción de ruido: Acoustic treatments for urban installations
-
Control del polvo: Advanced sealing and suppression systems
-
Recyclable Components: Sustainable material selection
Rumbos del mercado
-
Mayor automatización: Reduced human intervention requirements
-
Diseño modular: Faster installation and configuration changes
-
Normas globales: Uniform safety and performance requirements
-
Personalización: Application-specific engineering solutions
Belt conveyor technology continues to be the workhorse of modern material handling, providing reliable, efficient transportation across virtually every industrial sector. Their evolution from simple mechanical systems to sophisticated, integrated solutions reflects the ongoing demands for increased efficiency, reduced environmental impact, and enhanced operational intelligence. As industries continue to prioritize automation and sustainability, belt conveyors will remain essential infrastructure, continually incorporating new technologies to meet evolving operational requirements.
Reseñas
Todavía no hay reseñas.